-
WhatsApp +86 15116118247
-
Any Questions info@terrahats.com
Why Visual Inspection Alone Can Miss Hat Defects
Use a straw hat QC framework that checks identity, dimensions, construction, branding, function, labels and packing beyond appearance alone.

Quick answer
Visual inspection can reveal stains, deformation, loose threads, uneven printing, and damaged packing. By itself, however, it cannot confirm the correct head opening, brim width, component attachment, closure operation, SKU label, carton quantity, or other specified characteristics. It should be one part of a broader straw hat QC checklist.
A practical pre-shipment framework checks seven areas:
- Product identity
- Measurements
- Construction
- Branding
- Function
- Labels
- Packing
Each check needs a requirement, method, approved reference, and recorded result. If sampling is used, document the complete sampling plan; an AQL value alone does not explain how to reproduce the inspection or make the lot decision.
Table of Contents
Why a good-looking hat can still be nonconforming
A natural-straw sun hat may have an even weave, clean logo, undamaged crown, and no obvious stain—and still be wrong for the order. Compare that good-looking hat with the purchase specification:
- The order calls for a particular style and colorway.
- The head opening must follow the approved size specification.
- The brim must be measured using an agreed method.
- The logo must sit at a defined position.
- The chin cord and adjuster must operate as intended.
- The sewn-in label must match the assigned SKU.
- The unit must be packed in the approved orientation and quantity.
Several of these requirements cannot be confirmed reliably from appearance. ISO conformity-assessment guidance treats inspection as broader than looking: it can include visual examination, measurement, testing, document review, comparison with requirements, and reporting. NIST likewise defines testing as determining characteristics according to a procedure. The goal is to use the right evidence for each requirement, not to replace judgment with instruments.
Practical rule: If a requirement contains a number, operating condition, identity code, or hidden interface, define how to verify it. Do not assume appearance is enough.
The inspection matrix: check, method, reference, result
The matrix below is a framework, not a universal standard. The exact methods and acceptance criteria should be agreed for the product, material, construction, intended use, and order.
| Inspection area | What a visual check can reveal | Additional method where relevant | Comparison reference | Result to record |
|---|---|---|---|---|
| Identity | Obvious style or color mismatch | Match purchase order, SKU, colorway, size and component list | Approved order specification and item master | Correct item, mixed item, or discrepancy |
| Measurements | Gross distortion or asymmetry | Measure defined points using specified tools and conditioning rules | Dimension sheet and approved measurement method | Actual value and pass/fail against agreed tolerance |
| Construction | Loose threads, skipped stitches, visible cracks, weave breaks or poor finishing | Examine seam path and attachment; apply an agreed mechanical test if required | Approved sample, construction sheet and applicable test method | Defect type, location and test result |
| Branding | Obvious color, position or artwork problems | Measure placement; compare artwork version, logo size and application method | Approved artwork, placement diagram and sample | Version, position, dimensions and appearance result |
| Function | Missing parts or visibly damaged hardware | Operate closures, adjusters, chin cords, snaps or other components using a defined procedure | Functional requirement or approved sample | Operates, does not operate, or requires review |
| Labels | Missing or visibly crooked label | Verify SKU, size, fiber/care text, barcode and language against controlled data | Approved label file and order specification | Correct, incorrect, unreadable or missing |
| Packing | Crushed units, open cartons or visible moisture damage | Count units, confirm assortment, carton marks, orientation and protective materials | Packing specification and shipping documents | Quantity, assortment, carton condition and variance |
The instruction should also identify the inspector, timing, lot, sample-selection method, response to nonconformity, and retained evidence.
1. Identity: confirm that it is the right product
The hat may be well made but belong to the wrong SKU, size, colorway, market, or purchase order.
A visual check might catch a navy hat where beige was ordered. It may not catch:
- two similar natural-straw colorways mixed in one lot;
- an adult and youth size made with nearly identical styling;
- an earlier logo revision used on otherwise correct hats;
- the correct front badge combined with the wrong inner label;
- a carton containing the wrong size ratio;
- components approved for another order.
The inspection reference should identify the purchase order, product code, approved colorway, size, artwork revision, component list, and packing configuration. For example, two resort orders may use the same wide-brim design but differ by one line of logo text. Both can look professionally finished; the inspector must still match each version to its SKU and carton assortment.
2. Measurements: define the method before measuring
A brim can look balanced while measuring differently at defined points. A head opening can look correct but fall outside the agreed size requirement. Crown height, band width, logo position, binding width, and chin-cord length may also need measurement.
Reliable dimensional checks require more than a tape measure being present. The team should define:
- the measurement points;
- the hat’s condition and orientation during measurement;
- whether the product should be relaxed, shaped, or conditioned first;
- the tool used;
- the unit of measurement;
- the agreed tolerance;
- how rounding is handled;
- how the value is recorded.
Natural straw is a hygroscopic plant material: its fibers absorb and release moisture as relative humidity changes. This can cause the fibers to swell or shrink by different amounts along different directions, which may produce small changes in the dimensions or shape of a woven brim, crown, or head opening. For more repeatable QC results, avoid measuring hats immediately after exposure to unusually dry or humid storage or transit conditions. Where conditioning is relevant, allow the samples to stabilize in the temperature and relative humidity defined by the agreed measurement or test method, and record those conditions with the results. ISO 139 provides standard conditioning atmospheres for textiles, but its applicability should be confirmed for the specific straw material and hat construction rather than assumed for every order.
ISO 10012:2026 states the broader principle that measurement processes and equipment should produce valid, reliable, fit-for-purpose results. It does not set hat tolerances; those remain product-specific. If one inspector follows a flexible inner curve while another measures a flattened opening, their results are not comparable. A measurement diagram and written method remove that ambiguity.
3. Construction: check more than the surface
Visual inspection can find open seams, skipped stitches, loose threads, edge damage, visible adhesive, cracked straw, weave gaps, distorted panels, and poor binding. It cannot prove that a neat-looking attachment is secure. A patch may sit flat while its edge attachment is incomplete, or a decorative band may be aligned but insufficiently secured.
Where construction performance matters, the buyer and supplier should define an appropriate check. Depending on the design, that could be a specified seam examination, an attachment test, or another product-relevant method. The method must suit the material and geometry.
For context, ISO 13935-2:2026 specifies a machine-based method for testing certain straight sewn seams. It shows that seam properties can require mechanical testing, but it is not a universal hat test. Curved seams and other constructions may need a different approach.
The safe procurement question is not “Do you pull-test every hat?” It is:
Which construction characteristics require more than visual examination, and what agreed method is appropriate for this design?
4. Branding: verify the approved artwork, not just its appearance
“Logo looks good” does not answer:
- Is this the approved artwork revision?
- Is the logo the agreed size?
- Is it positioned from the correct datum?
- Is the patch material correct?
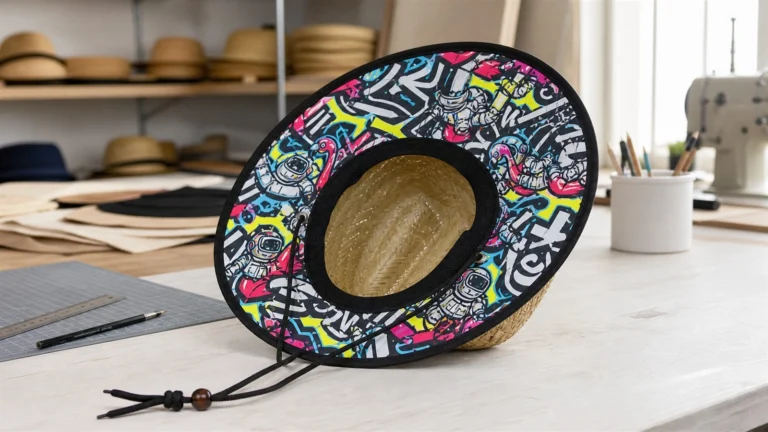
- Is the under-brim print oriented correctly?
- Is the thread, ink, or patch color being compared under suitable lighting?
- Is the branding method the one approved for this SKU?
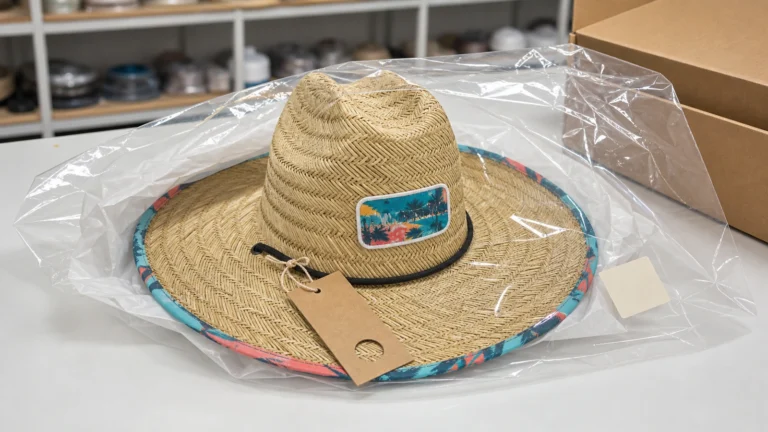
Natural fibers and textured surfaces interact with weave, curvature, and substrate color, so a physical approval reference and controlled artwork are especially useful. A front patch may appear centered but measure off-position from the approved construction datum. Branding inspection should combine appearance review with file identity, dimensions, placement, material, and application-method checks without promising identical results across natural surfaces.
5. Function: operate the components
Functional defects may remain hidden until someone operates the product.
Relevant checks depend on the hat design. They may include:
- a chin-cord adjuster moving and holding as specified;
- a snap closing and reopening;
- a hook-and-loop or buckle adjustment engaging correctly;
- a removable component attaching in the intended orientation;
- a foldable design recovering in the way described by its approved requirement;
- an internal feature sitting correctly when the hat is worn.
A component can be present and undamaged yet still bind, slip, detach, or operate inconsistently. Define the check before inspection: “test the buckle” is less useful than a short procedure stating how to operate it, the expected outcome, and the result to record. If force, cycles, or conditioning matter, agree on those parameters too. Avoid improvised final-inspection tests that may damage goods or produce results that cannot be compared.
6. Labels: check the data as well as the print
Labels sit inside the product or on packaging, so a general top-down visual review can miss them.
A label check may need to cover:
- brand and product identity;
- size;
- SKU or style code;
- barcode data and readability;
- fiber or care wording where applicable;
- country or market-specific content where required;
- label position and orientation;
- hangtag-to-product matching;
- carton mark consistency.
Use the approved label file or controlled order data—not an inspector’s memory or a similar previous product. A sharp-looking label can still carry the wrong size, barcode, language, or revision. Record appearance and data accuracy separately. Barcode scanning or controlled data comparison can catch a polished hangtag assigned to the wrong colorway before receiving or retail allocation.
Legal labeling obligations vary by product and destination. The buyer should identify applicable requirements with qualified compliance support rather than treating this general QC framework as legal advice.
7. Packing: protect the approved product after inspection
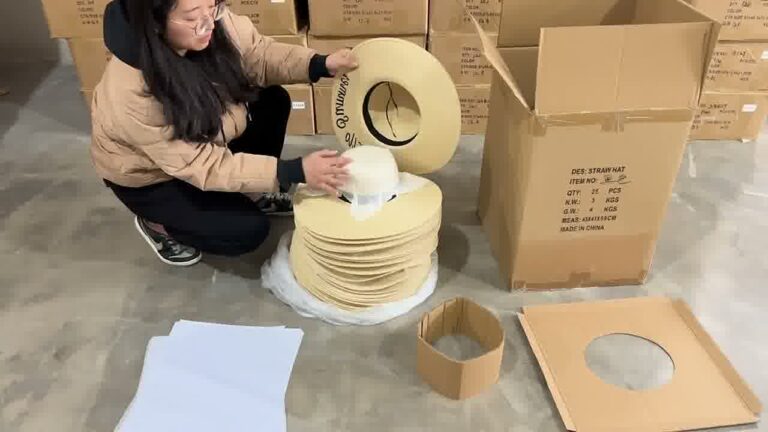
A finished hat can pass product checks and still arrive with problems if the packing method is wrong.
Visual carton inspection can reveal crushing, holes, water marks, open seals, and poor external condition. A complete packing check may also need to verify:
- units per inner pack and carton;
- size and color assortment;
- nesting or orientation;
- shape supports or protective materials;
- individual bag or retail-pack configuration;
- carton dimensions and weight records where specified;
- carton marks, purchase-order references, and destination data;
- separation of different SKUs;
- agreement between packed quantity and shipping documents.
Wide brims, structured crowns, ornaments, and natural materials respond differently to pressure and nesting. Approve the method for the actual product instead of copying another hat’s specification. Even when the unit and carton count are correct, the wrong nesting direction can place repeated pressure on a trim component.
What an AQL plan does—and what it does not do
Acceptance sampling uses a sample to support a decision about whether to accept or reject a lot. NIST describes it as a middle path between no inspection and examining every unit. Its purpose is lot disposition, not calculating the shipment’s exact quality level.
The current ISO reference is ISO 2859-1:2026, Edition 3. It describes AQL-indexed sampling schemes for inspection by attributes, including single, double, and multiple plans and switching among inspection states.
Two cautions matter. First, an AQL does not guarantee a defect-free shipment. Sampling carries statistical risk: an acceptable lot can be rejected, and an unacceptable lot can be accepted. Second, an AQL value is not a complete plan. The instruction also needs the lot size, inspection level, sampling form and state, sample size, acceptance and rejection numbers, selection method, defect definitions, and decision rules.
Define defect categories before inspection according to product risk and buyer priorities; a generic checklist cannot classify an issue as critical, major, or minor for every program. If a report uses AQL language, ask for the documented plan rather than relying on the label.
Buyer checklist: build a QC brief before production
Use these questions when preparing a sample approval, purchase specification, or pre-shipment inspection brief:
- Are all styles, colors, sizes, and artwork revisions linked to unique product identities and the current purchase order?
- Does the team have the approved physical sample, controlled digital reference, or both?
- Are measurement points, methods, tools, units, and tolerances defined?
- Are acceptable natural-material variations described without promising exact uniformity?
- Are construction details, attachments, and any non-visual methods documented?
- Are the approved logo revision, size, placement, material, and application method specified?
- Are functional procedures repeatable, with expected outcomes and records defined?
- Are label files, barcode data, sizes, SKUs, and destination-specific questions controlled?
- Is the packing configuration approved, including quantities, assortments, marks, orientation, and protection?
- Is the inspection lot identified and, if sampling is used, is the complete plan documented?
- Are defect definitions connected to product requirements?
- Does the report record findings, discrepancies, review, disposition, photos, measurements, and packing evidence?
A checklist only needs enough detail for the buyer, supplier, and inspector to check the same product against the same evidence.
Frequently asked questions
Is visual inspection still useful for hat QC?
Yes. Visual inspection is efficient for observable workmanship and condition, including stains, deformation, loose threads, obvious weave damage, print problems, and visible packing damage. It becomes unreliable when it is expected to prove dimensions, operation, identity, attachment performance, or hidden details without another suitable method.
What should be included in a straw hat QC checklist?
At minimum, include identity, measurements, construction, branding, function, labels, and packing. For each area, state the requirement, inspection method, reference, and result to record. Add product-specific checks according to the material, construction, intended use, and buyer risk.
Does passing an AQL inspection mean every hat is defect-free?
No. Acceptance sampling supports a statistical decision about a lot based on a sample. It does not prove that every unit is conforming or reveal the shipment’s exact defect percentage.
Is an AQL value enough to tell an inspector how many hats to check?
No. The sample size and decision criteria depend on more than the AQL. The instruction also needs information such as lot size, inspection level, sampling form, current inspection state, and the relevant acceptance and rejection rules.
Should every hat receive the same tests?
No. The check must fit the product and requirement. A straw sun hat, fabric cap, structured fedora, and hat with removable components may need different methods. A test can also be inappropriate if its material or geometry falls outside the method’s scope.
Can an approved sample replace a written specification?
An approved sample is valuable, especially for appearance, hand feel, construction, and branding context, but it does not replace controlled written information. Measurements, component identities, artwork versions, label data, packing quantities, and agreed methods are easier to reproduce when documented.
Who should define acceptable hat defects?
The buyer and supplier should agree on requirements and defect definitions before inspection, with qualified testing or compliance support where necessary. A third-party inspector can apply a defined plan, but should not have to invent the commercial or safety criteria at the inspection table.
Make the inspection match the order
The most expensive quality problem is not always the most visible one. A hat may look good and still be the wrong size, carry the wrong label, use the wrong artwork revision, contain a non-operating component, or enter the carton in the wrong assortment.
A stronger QC process starts with the order specification. It then assigns the right evidence to each requirement: visual examination for appearance, measurement for dimensions, defined procedures for function, controlled records for identity and labels, and an applicable sampling plan for lot decisions.
Visual inspection remains essential. It simply should not be asked to answer questions it cannot answer on its own.
To organize specifications, inspection references, and packing requirements for a custom hat program, visit the TerraHats factory page or contact TerraHats. Share the hat style, order structure, quality concerns, and existing inspection requirements for review against a defined brief.
CMS lead-magnet note: Replace or supplement this CTA only after the planned Pre-Shipment QC Checklist has been completed, verified, uploaded, and assigned a working destination. Do not add a placeholder download URL.
Sources and further reading
- ISO 2859-1:2026 — Sampling procedures for inspection by attributes
- ISO CASCO — Conformity assessment techniques and schemes
- ISO/IEC 17000:2020 — Conformity assessment vocabulary and principles
- ISO 10012:2026 — Measurement management systems
- ISO 139:2005 — Standard atmospheres for conditioning and testing textiles
- ISO 13935-2:2026 — Seam tensile properties using the grab method
- Canadian Conservation Institute — Caring for basketry and plant materials
- NIST — Inspection
- NIST — Testing
- NIST Engineering Statistics Handbook — What Is Acceptance Sampling?
- NIST Engineering Statistics Handbook — Types of Lot Acceptance Sampling Plans
- NIST Engineering Statistics Handbook — Choosing a Sampling Plan